Friday Fun: The Product Was Finished. Unfortunately, the Material Was Not.
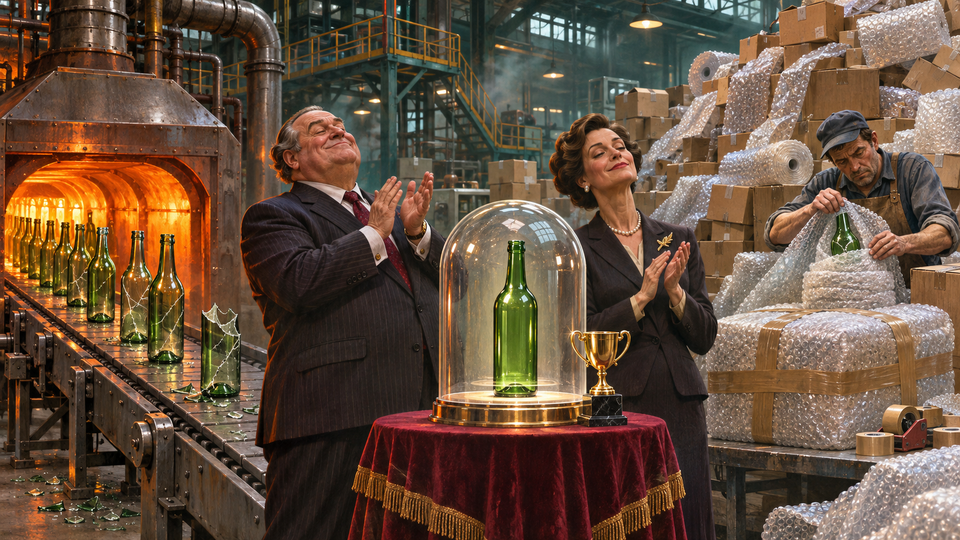
A bottle with unfinished business
Watch a bottle take shape and the decisive moment seems obvious. The glowing glass enters a mould, expands into the cavity and emerges with a body, shoulders and a neck. Something that recently looked incapable of holding its own shape now looks capable of holding wine. For anyone standing beside the line with a sales forecast, the remaining work appears largely logistical.
The bottle, however, still carries the thermal consequences of its manufacture. Glass expands when heated and contracts when cooled. Different parts of an object can cool at different rates, particularly where thickness varies. As the material passes into a more rigid condition, uneven contraction can leave internal stresses behind. A bottle can therefore possess the correct dimensions while carrying a less visible inheritance from the process that produced it. The Corning Museum of Glass notes that inadequately annealed objects may break during cooling or later, and become particularly vulnerable to thermal or mechanical shock.
This explains the long tunnel that follows the more theatrical business of forming. An annealing lehr moves glass containers through a controlled temperature profile, allowing stress relief and gradual cooling. Its contribution lacks the spectacle of a furnace or a forming machine. Bottles enter looking like bottles and leave looking like bottles. Considerable engineering has occurred in between, but the silhouette offers disappointingly little material for a launch video.
The suspicious absence of visible progress
Annealing requires more thought than leaving hot objects somewhere until they feel approachable. The glass must reach suitable thermal conditions for stresses to relax, then cool through the critical range without acquiring unacceptable new stresses. The appropriate schedule depends on composition, shape and thickness. The temperature indicated by an instrument does not automatically establish that every part of the object has reached the same condition.
Nor does this mean that slower always means better, or that an inherited schedule deserves eternal protection. Research into bottle annealing explicitly examines how thermal cycles can be calculated and optimised. The engineering question concerns the condition of the glass produced by a particular cycle. A shorter process can represent an improvement when its thermal behaviour supports it. A shorter process justified by the approaching end of the quarter requires a different branch of physics.
Inspection also extends beyond admiring an intact object. A polariscope uses polarised light to reveal stress patterns that ordinary viewing conceals. Scientific glassblowers use it to compare work before and after annealing. The object has not changed its external design, yet the instrument can reveal something consequential about its internal condition. Looking finished and having completed the necessary transformations belong to different categories of evidence.
There is an unfortunate presentational imbalance here. Forming produces a visible achievement. Annealing produces a reduced probability of an unwelcome event. One photographs beautifully. The other asks somebody to remain interested in a bottle that continues, rather uneventfully, to exist.
The tunnel enters its performance review
Imagine a fictional factory in which this distinction attracts a productivity programme. Its glass obeys ordinary physics, while its reporting arrangements permit greater creative freedom. A review identifies the lehr as a substantial interval during which products travel slowly without acquiring additional features. The forming machine delivers a bottle. The tunnel then takes an unreasonable amount of time to deliver the same bottle, slightly colder.
Nobody proposes removing the tunnel. The programme simply gives it a shorter target cycle before establishing which thermal changes would support one. An external benchmark supplies the target, although the comparison factory’s bottle geometry remains unavailable. Requesting those details would delay implementation. The benchmark has already demonstrated its value by allowing everyone to agree on a number.
An operator explains that the thicker base cools differently from the wall. The programme records this as resistance to change and arranges a workshop in which the operator can feel heard while the belt runs faster. The base receives no invitation. It continues conducting heat at the old rate, displaying precisely the inflexibility associated with legacy manufacturing.
The revised schedule reduces time in the lehr, allowing bottles to reach packing earlier. Whether the whole plant can sustainably produce more requires a wider examination, but the project measures tunnel transit time, so that complication falls outside scope. Photographs establish that the bottles have retained their necks. Internal stress has no column in the dispatch report and shows commendable discretion during the award ceremony.
Customer success learns to sweep
The first complaints arrive from elsewhere. Some containers fail during handling or filling, when additional mechanical or thermal loads expose their vulnerability. They do not all fail together. Different histories of handling and temperature produce a scattered pattern, which helps the factory describe each occurrence as an isolated incident. There are enough isolated incidents to justify a dedicated team.
Dispatch confirms that the goods left intact. Logistics confirms that the shipment followed the agreed route. Production notes that bottles have always required careful handling. Customer support receives the only indisputable new requirement: more customer support. Its team expands the troubleshooting guide to include room temperature, filling temperature and the possibility that the customer has introduced liquid.
A cross-functional group develops a leaflet entitled Getting the Best from Your Bottle. Customers should avoid abrupt movements, unsuitable surfaces and excessive confidence. A short instructional video demonstrates successful handling under conditions approaching those of a museum collection. Anyone still experiencing breakage can attend a webinar on responsible ownership.
By the time complaints accumulate, the productivity review has closed. The bottles crossed the reporting boundary before their consequences crossed back. Lost filling time belongs to the customer, returns belong to quality, and the investigation belongs to next quarter. The improvement remains in the quarter in which it occurred, where nobody can get at it without restating the presentation.
The department of retrospective explanation
A growing collection of fragments eventually makes the thermal cycle difficult to ignore. Quality requests a review. Restoring adequate processing conditions now threatens more than the transit-time target. The shorter cycle has entered forecasts, commercial promises and the next budget. A decision originally justified as an experiment has acquired dependants. Reversing it would require several departments to revise numbers they have already described as commitments.
The investigation therefore needs a cause that can be corrected without disturbing those commitments. Packaging offers an attractive starting point. Protective material can reduce damage from handling, and its budget belongs elsewhere. It cannot anneal the bottles, but it can make the programme’s continued existence easier to defend. The business purchases more cardboard to preserve the saving on time.
Training follows. Handlers receive courses, supervisors receive checklists and suppliers receive questionnaires. None of these activities looks absurd on its own. Fragile goods need protection, people need information, and complaints need investigation. Their combined cost exceeds the original saving, but no single budget contains that discovery. The company has distributed the answer so successfully that every department can afford its own explanation.
The polariscope presents a more delicate difficulty. Under ordinary light, the bottle looks acceptable. Under polarised light, the inconvenient patterns appear. A working group examines whether the instrument reflects representative customer conditions, since most customers do not drink through polarising filters. Until that question receives an answer, the findings remain technically interesting but commercially premature.
When time gets charged to the wrong place
Software has its own less tangible versions of the cooling tunnel. A feature may satisfy its demonstration while the organisation still lacks tested recovery procedures, an understood support model or evidence about its behaviour under representative load. These activities differ from annealing and cannot share a universal timetable. They do share the inconvenience of producing changes that a screenshot cannot establish.
A release can consequently move faster without the necessary work disappearing. That work returns through incidents, support requests and manual interventions, often involving people outside the team credited with delivery. The organisation then observes that development has accelerated while operations has become inefficient. A transformation programme examines why operations keeps interrupting the people who have already finished.
The comparison has limits. Engineering can remove genuine waste, and neither glassmaking nor software benefits from preserving every inherited delay. A better thermal design may support a shorter cycle. A different software design may remove the need for a manual check. The reduction becomes credible through a changed process and evidence about its results. A deadline supplies neither, however prominently it appears on the factory wall.
Our fictional factory prefers a simpler arrangement. Every additional activity after dispatch belongs to the customer experience. This classification allows the production team to remain proud of its improved efficiency while the support team works towards a maturity assessment. The bottles connect both departments more effectively than their reporting lines do, usually by breaking.
The premium range requires patience
Eventually, sales proposes a premium bottle for customers who have expressed a preference for containers that remain containers. The new range passes through a revised thermal cycle, validated against its actual geometry and expected use. It costs more, partly because the company has rediscovered an operation previously removed from the standard offering.
Marketing describes the result as enhanced structural confidence. The brochure avoids dwelling on what confidence means for purchasers of the ordinary range. Finance approves the differentiation because the additional processing time now carries a price rather than appearing as a delay. The same duration that obstructed productivity becomes commercially attractive once customers can pay separately for its consequences.
Meanwhile, the standard line retains its faster schedule. Packaging has negotiated a volume discount, customer education has a quarterly attendance target, and the breakage team has recruited a manager. Restoring the thermal cycle would now reduce demand across several apparently successful functions. The tunnel’s missing minutes have become somebody else’s revenue, staffing case and promotion opportunity.
At the annual review, the premium bottle stands beside the productivity award. Slides celebrate shorter cycles, service growth and a successful move into higher-value products. Beyond the conference-room wall, glass travels through the longer tunnel at the rate its temperature profile permits. The award has meanwhile been placed in a protective display case. Purchasing obtained the glass from another manufacturer
Member discussion